DTF / No-Cut Printing
Full-colour artwork, gradients, photos and small to medium runs on cotton, polyester and blended garments.
Best for
Detailed logos, merch drops, school events, mixed sizes
Low to medium quantities
DTF and heat transfer printingBranded T-shirts for your team, event or next merchandise release. Choose a garment, share your artwork and find the right print or stitched finish for the job.
DTF, screen printing, sublimation, embroidery and vinyl. Garment, sizes, quantity and artwork are confirmed for your order.


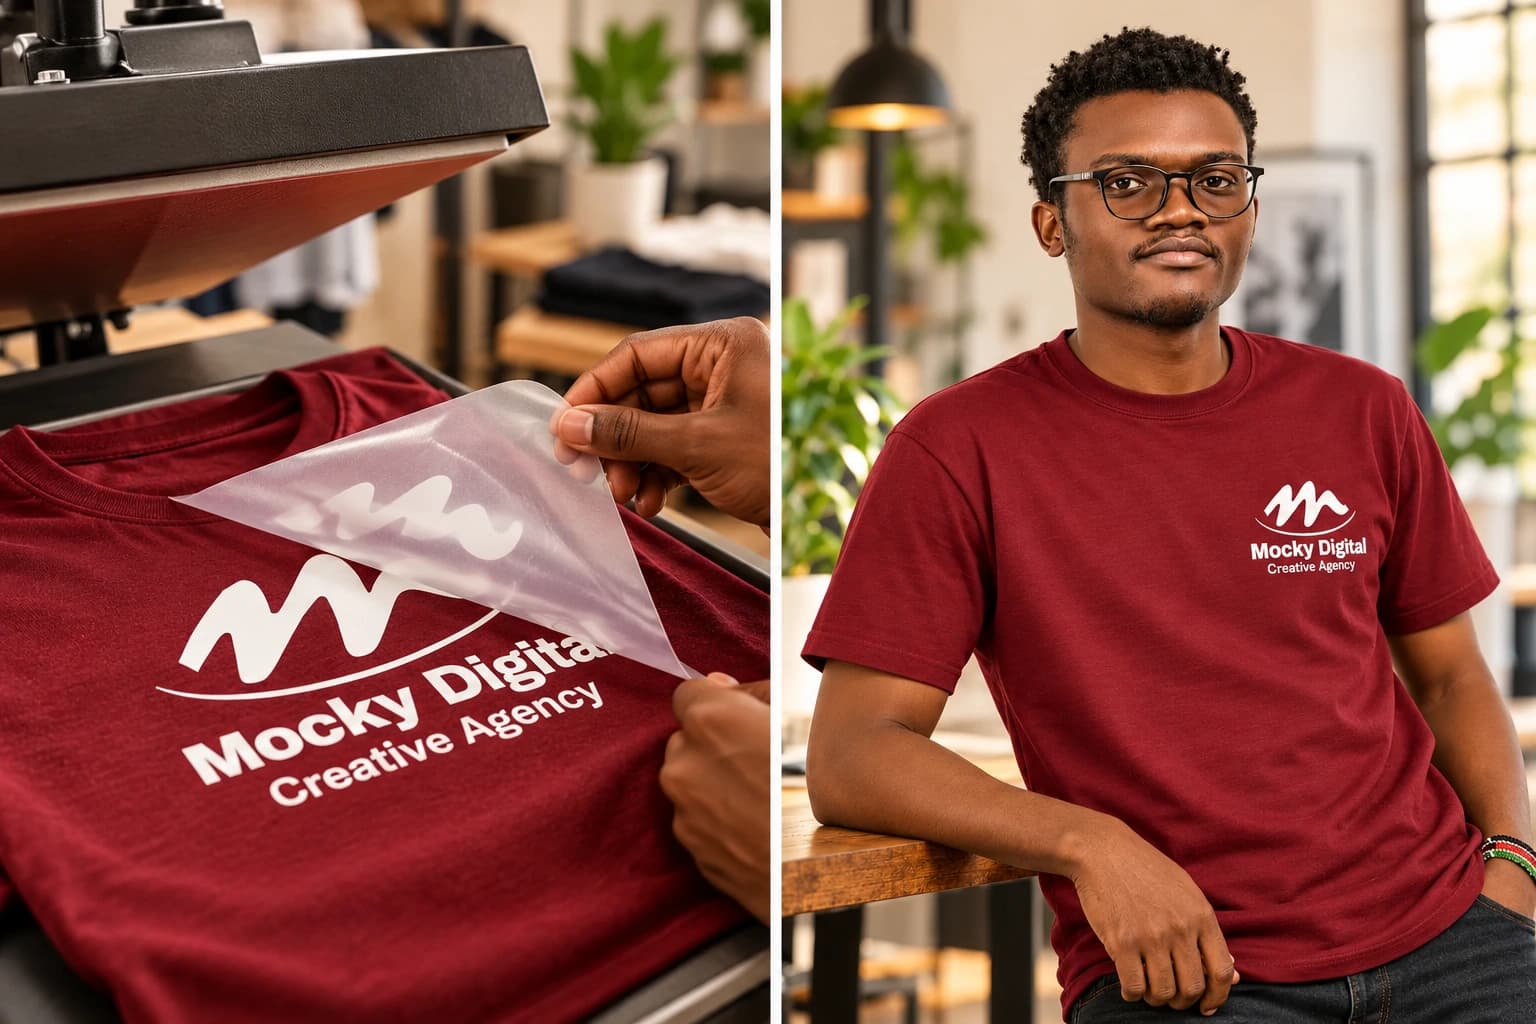
See how each method is applied and how the finished garment looks when worn. We’ll help you choose based on your artwork, fabric and order size.

Full-colour artwork, gradients, photos and small to medium runs on cotton, polyester and blended garments.
Best for
Detailed logos, merch drops, school events, mixed sizes
Low to medium quantities
DTF and heat transfer printing
Durable and cost-effective for bulk T-shirts with bold designs, limited colours and repeatable artwork.
Best for
Corporate events, NGOs, campaigns, schools, uniforms
Best value from bulk runs
Screen printing in Nairobi
Vibrant dye print for polyester sportswear and full-panel designs that should not crack or peel.
Best for
Jerseys, sports teams, all-over prints, marathon kits
Project dependent
Sublimation printing in Kenya
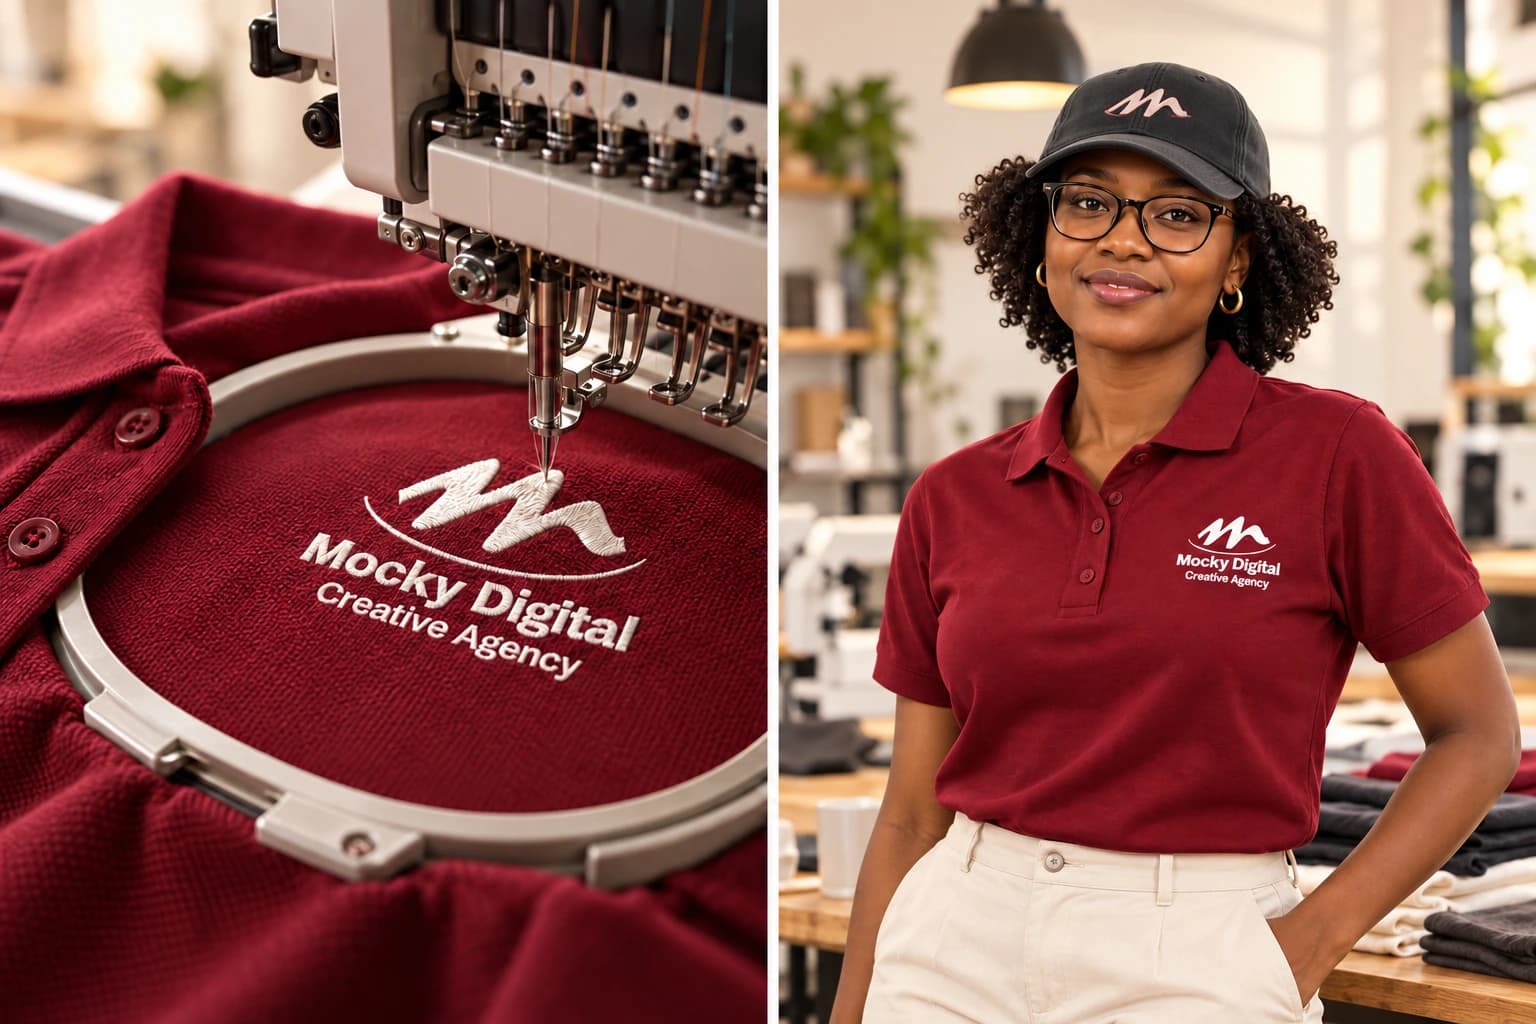
Premium stitched branding for polos, caps, jackets and uniforms where durability and a corporate finish matter.
Best for
Polo shirts, executive uniforms, caps, hospitality teams
Logo digitizing may apply
Embroidery services in Nairobi
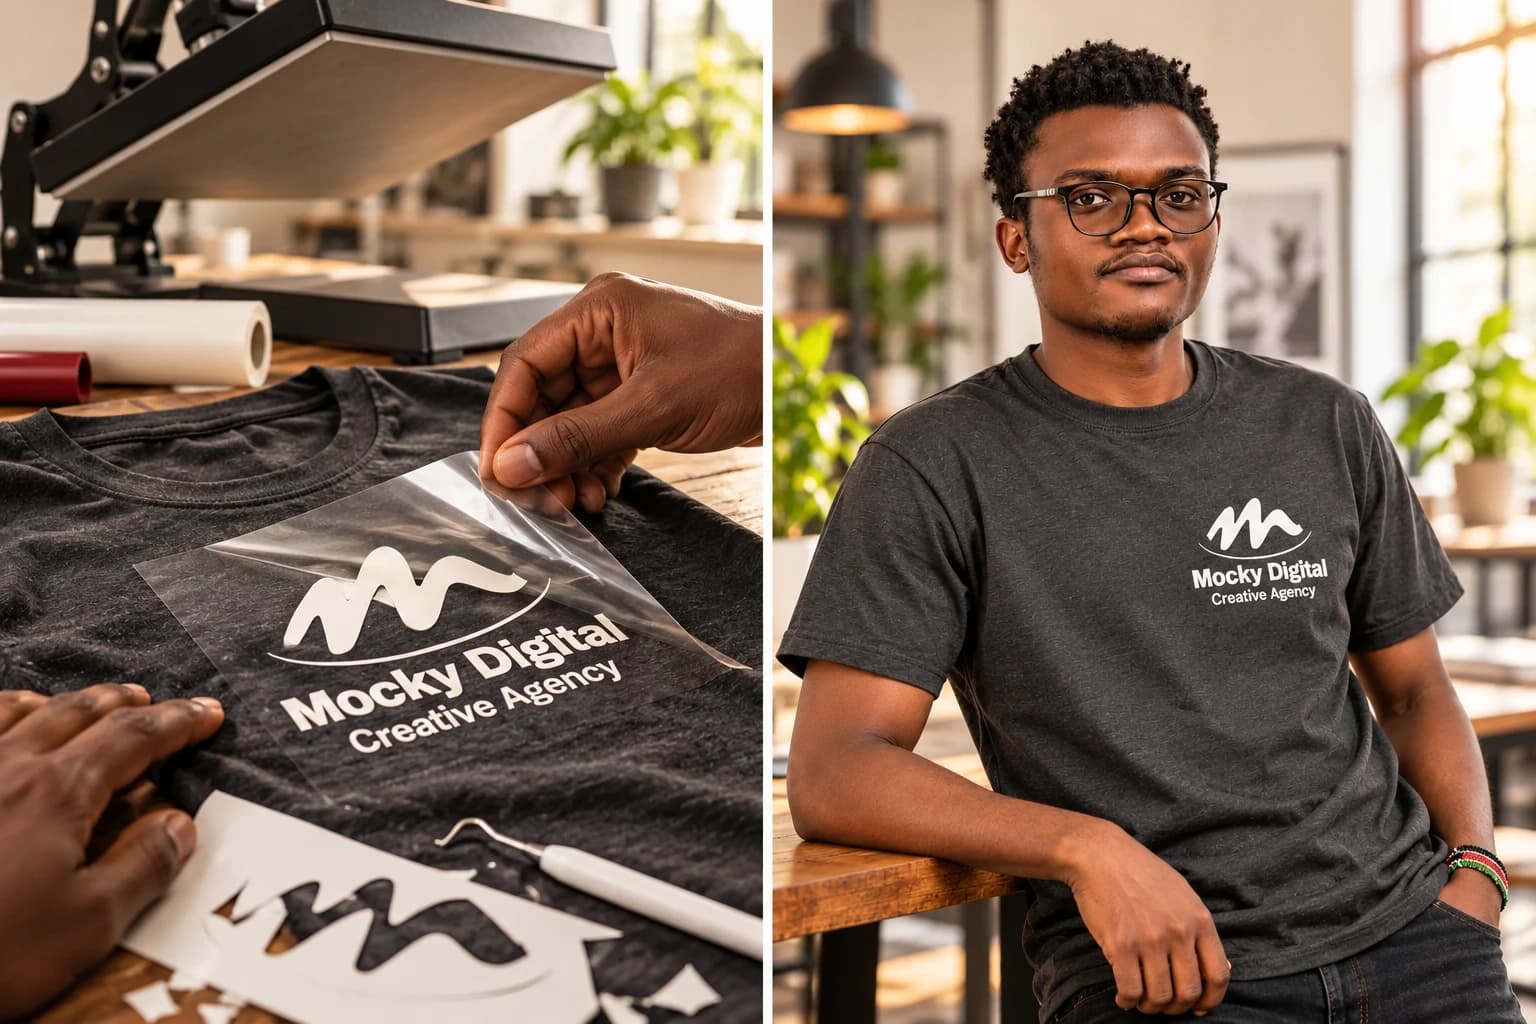
Clean names, numbers and simple graphics for jerseys, staff shirts and personalised one-off apparel.
Best for
Names, numbers, reflectors, single-colour marks
Small runs and personalisation
Vinyl and heat transfer printingFrom company uniforms to branded event merchandise, the practical difference is in the print method, file quality, sizes and production timing. Send your quantity and deadline early if the job is urgent.
Corporate uniforms and branded staff T-shirts
Event T-shirts for churches, schools, NGOs and conferences
Campaign T-shirts for launches, activations and roadshows
Sports jerseys, team kits and marathon shirts
Merchandise for creators, artists and fashion drops
Promotional giveaways for expos, sales teams and retail campaigns

Branded hoodies for staff, events, creators and team merchandise. Choose a subtle embroidered chest logo or a larger printed design, then coordinate the colours, sizes and placement across the order.
Share the hoodie fabric, quantity, logo file and preferred positions. We’ll confirm whether printing or embroidery suits the item before quoting.

Compare a smaller stitched chest mark with a larger printed design. Keep the logo clear of pockets and seams, and choose a thread or print colour with enough contrast against the hoodie fabric.
Explore the details before ordering, including screen printing in Nairobi, DTF and heat transfer, and sublimation printing in Kenya. Sublimation also covers suitable coated mugs, not only clothing. Share the exact item so we can confirm its compatibility.
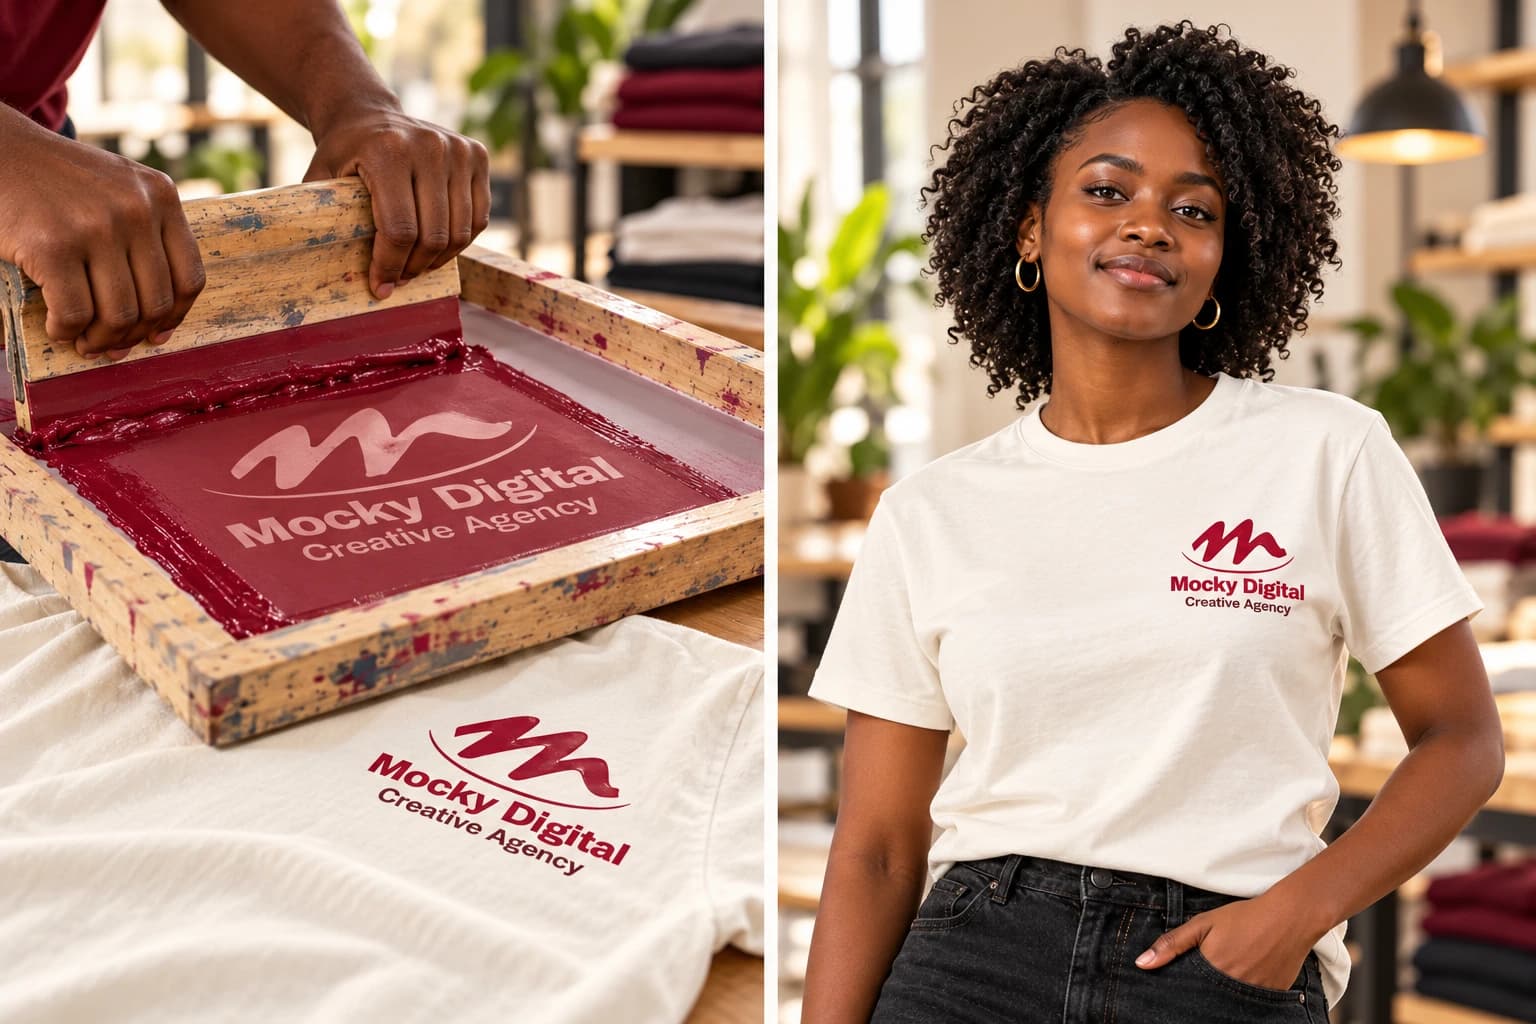
The most economical way to brand a large run. Ink pushed through a screen, one screen per colour, priced so the cost per piece falls as the quantity climbs.
Number of colours in the design. This is the dominant factor. Every colour needs its own screen, its own set-up and its own pass through the press. A one colour logo is dramatically cheaper to run than a five colour one, at any quantity.
Quantity. Screen set-up is a fixed cost that happens once per colour, no matter how many shirts follow. Spreading it over 500 pieces instead of 30 is what makes screen printing cheap in bulk, and it is why the cost per piece drops steeply as the order grows.
Number of print positions. Front and back are two separate runs, each with its own screens and set-up. A chest print plus a back print is effectively two jobs on the same garment.
Garment colour. Printing light ink onto a dark garment needs a white underbase printed first so the colours stay bright. That is an extra screen and an extra pass, so the same design costs more on black than on white.
Print size. Larger prints use more ink and need larger screens and more press time. An A3 back print costs more to run than a small left chest.
Ink type and finish. Standard plastisol covers most jobs. Water based and discharge inks give a softer feel, and puff, metallic and glow inks are specialty finishes. Each of these changes both the material cost and the handling.
Artwork separation. Artwork has to be separated into one layer per colour before screens can be made. Clean vector art separates quickly. Photographic or heavily blended art needs halftone or simulated process separation, which is more work and more screens.
Vector artwork, colours separated. AI, EPS, PDF or SVG with each colour as its own clearly defined element. This is what makes screen output fast and accurate.
Use spot colours, not gradients. Screen printing lays down solid spot colours. Send Pantone references where you have them so we can mix to match. Gradients and soft fades have to be converted to halftone dots, which changes how the design looks.
Keep the colour count deliberate. Because every colour adds a screen, reducing a design from five colours to two is usually the fastest way to cut the cost of a large run without hurting the look.
Flag photographic designs early. Photographs can be screen printed using simulated process, but it needs many screens and careful set-up. If your design is photographic, heat transfer is often the better and cheaper route, and we will say so.
Before anything is printed, a screen has to be made for each colour in the design and the press has to be set up and aligned. That work costs the same whether you print twenty shirts or five hundred. On a large run it is spread thin, which is why screen printing gets cheaper per piece the more you order.
Yes. Each colour is a separate screen, a separate set-up and a separate pass through the press. Going from one colour to four multiplies the preparation work. If a budget is tight, simplifying the design to fewer colours usually saves more than any other change.
It is possible using halftones or simulated process, but it needs a lot of screens and careful set-up, so it is rarely the economical choice. For photographic or full colour artwork we would normally recommend heat transfer printing instead.
Yes. Send the garments or the exact product details in advance so we can confirm the fabric takes the ink properly, and so we can plan the print size against the garment.
Full colour artwork printed onto film or cut from vinyl, then heat pressed onto the garment. The method that handles reflector jackets, dark workwear, bags and short runs.
Size of the print. DTF is priced by the area of film your design occupies. A small left chest badge uses a fraction of the film that a full back print does, so size is the main lever on cost.
Number of positions. Each position is a separate press. A chest logo, a back logo and a sleeve detail means the garment goes under the press three times, and each of those presses is priced.
Quantity. There are no screens to make, so there is no large fixed set-up to recover. That is why this method suits small runs. Volume still earns a better rate through faster handling, but the curve is much flatter than screen printing.
DTF or cut vinyl. DTF prints full colour artwork onto film, so the number of colours makes no difference to the price. Cut vinyl is a solid sheet cut to shape, and each additional vinyl colour is a separate cut and a separate press layer, so colour count does matter there.
The garment or substrate. Hi-vis, waterproof coated, heavily textured and technical fabrics all behave differently under heat. Some need a different adhesive, a lower temperature or a test press first. Tell us what the garment is and we will confirm the approach before quoting.
Personalisation. Individual names, numbers or codes mean every piece is a different transfer and a separate press. That adds per unit handling, which is priced differently from a batch of identical garments.
Ink coverage. Dense, solid blocks of colour use more ink and more white underbase than light line work of the same dimensions.
For DTF, send high resolution artwork at final size. A PNG with a transparent background at 300dpi at the size it will print is ideal. Vector is even better. DTF prints its own white underbase, so full colour artwork works on black, navy and hi-vis alike.
For cut vinyl, send vector only. Vinyl is physically cut, so the design must be solid shapes with clean outlines. Gradients, soft edges and photographic detail cannot be cut. AI, EPS, PDF or SVG.
Tell us the garment colour. It changes nothing about the file for DTF, but it does change how we set the white underbase, and it matters a great deal for how the finished design will read.
Send personalisation as a list. If each piece carries a different name, number or size, send it as a spreadsheet so nothing is mistyped between your list and the press.
Yes, this is the method for it. Reflector vests are usually a strong colour, and designs on them normally include white, which rules out sublimation. A heat applied transfer carries its own white, so full colour logos sit cleanly on lime, orange or navy hi-vis. Send us the vest type first so we can confirm the fabric and its coating take heat well.
DTF prints your artwork in full colour onto a film, so photographs and multi colour logos cost no more than a single colour one. Vinyl is a solid coloured sheet cut to the shape of your design, so it suits names, numbers and simple one or two colour marks, and each extra colour adds a layer.
A well applied transfer lasts a long time through normal washing, but on very large solid areas and heavy industrial laundering, screen printing and embroidery generally have the edge. For workwear that gets washed hard, we will tell you if embroidery is the safer choice.
Yes. Because there are no screens to prepare, small quantities and single pieces are practical with this method, which is the main reason to choose it over screen printing for a short run.
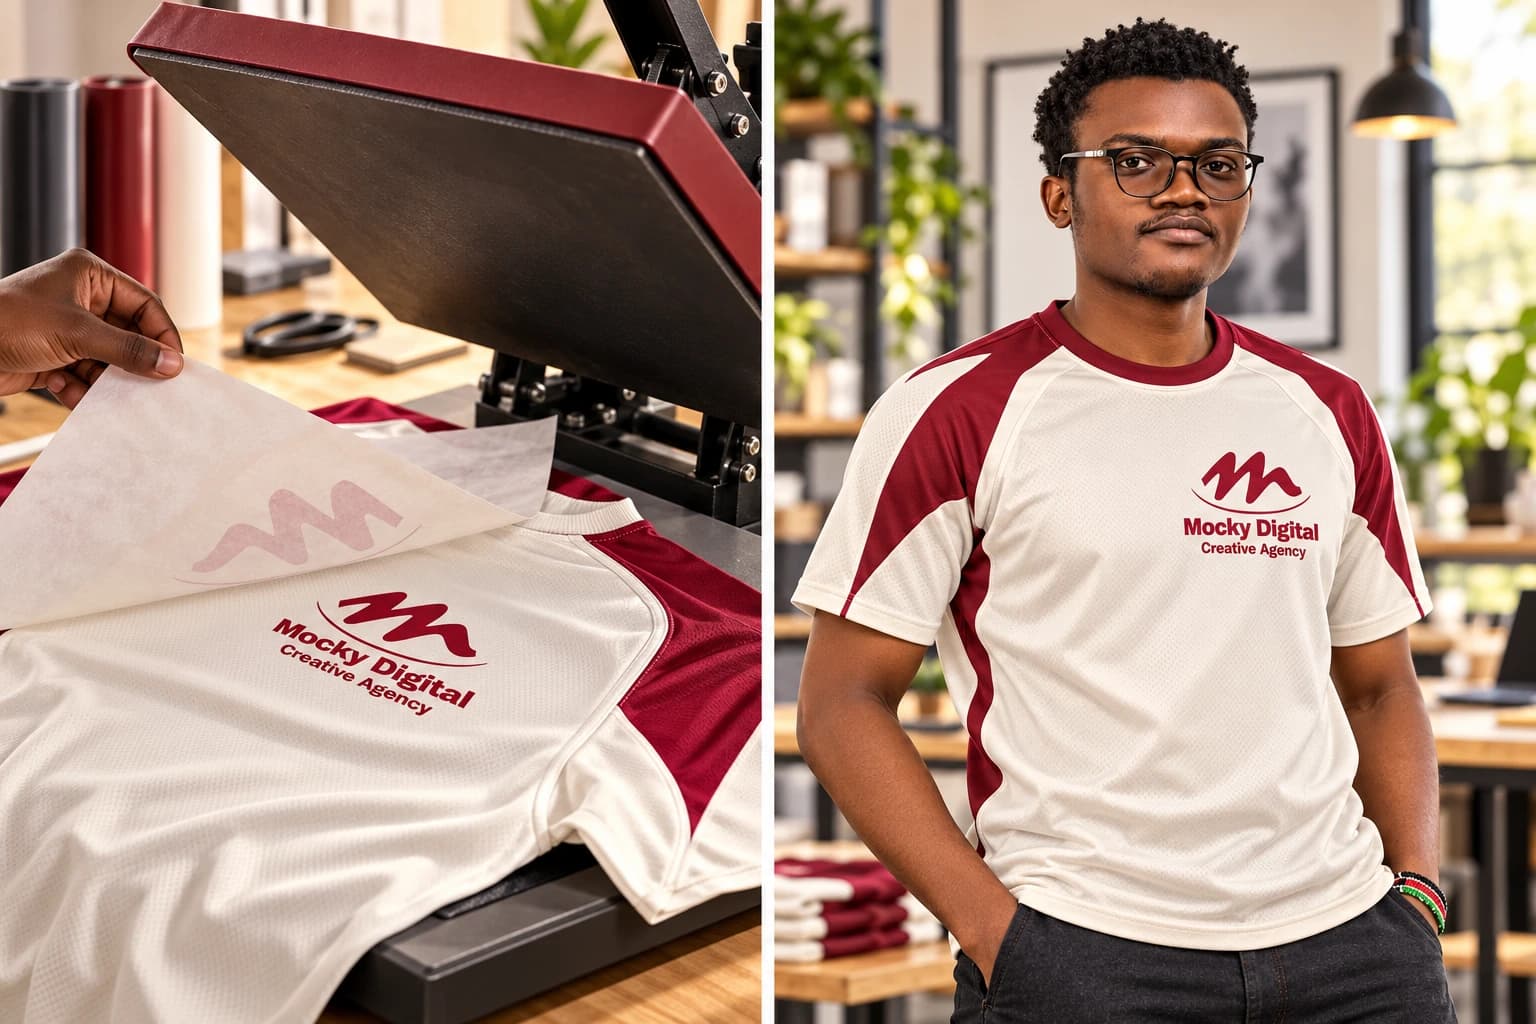
Dye that becomes part of the fabric. Nothing sits on top, so there is no weight, no cracking and no peeling. The right method for polyester jerseys, sportswear and mugs.
Coverage area. A small chest logo uses a fraction of the transfer paper and ink that a full all over print does. Coverage is the main driver, and an all over design that runs to the seams is the most expensive end of it.
Product type. Pressing a garment, a mug and a bottle are three different jobs with different jigs, temperatures and press times. Hard goods are priced separately from apparel.
Cut and sew or press onto finished garments. A true all over jersey is printed on fabric first and then cut and sewn into a garment, which is a far bigger job than pressing a design onto a shirt that is already made. The two are priced very differently, so tell us which you need.
Quantity. Set-up is modest compared with screen printing, so small runs remain practical. Larger runs still earn better rates through faster handling and more efficient use of material.
Fabric specification. Sublimation needs a high polyester content to bond properly. The higher the polyester, the stronger and more vivid the result. Blends with a lot of cotton print faded and wash out over time, which affects what we can quote and guarantee.
Number of positions or panels. Front, back and sleeves on a cut and sew jersey are separate printed panels. Each one adds material and press time.
High resolution, at final size. Send artwork at the dimensions it will print, at 300dpi. All over designs need to be supplied full bleed with extra margin beyond the seams so nothing important is lost when the panels are cut.
Remember that white is not printed. Sublimation has no white ink. Anywhere your design is white, the fabric itself shows through. That is why the garment has to be white or very light, and why this method cannot be used on reflector vests or dark shirts.
Design in CMYK and expect a slight shift. Sublimation colours are vivid but they do shift a little between screen and fabric. Send brand colour references and we will confirm the closest achievable match before a full run.
Confirm the garment fabric first. Before artwork matters at all, the garment has to be suitable. Send the product details or a sample so we can check the polyester content.
No, and it is worth being clear about why. Sublimation dye is translucent and it has no white, so it can only be seen on a white or very light base. On a lime reflector vest or a black shirt the design would not show. For those garments the right method is heat transfer printing, which carries its own white underbase.
Not properly. The dye bonds with polyester fibres, so it needs a high polyester content to hold. On cotton the print looks washed out from the start and continues to fade. If your garment is cotton, screen printing or heat transfer is the correct choice.
An all over jersey is printed as flat fabric and then cut and sewn into the finished garment, which is how designs run right to the seams with no gaps. A printed jersey is an existing garment with a design pressed onto it. The first gives full edge to edge coverage and costs more, the second is quicker and cheaper.
Yes. Poly coated hard goods such as mugs, bottles, mousepads and phone cases all take sublimation. They use different jigs and press settings from garments, so they are quoted separately.
Tell us what you need and the next decision you want help with. Your enquiry goes to the team handling this service.
Mocky Digital helps companies, teams and creators plan custom tshirt printing in Nairobi from the first artwork check to final delivery. We help you choose the right garment, print method, print position and quantity so the final shirts look consistent in photos, at events and in daily staff use.
Different artwork needs different production. DTF works well for detailed full-colour prints, screen printing is strong for bulk branded T-shirts, sublimation fits polyester sportswear and embroidery gives polos or caps a premium stitched finish. Browse Clothing & Apparel in our shop, or send your artwork on WhatsApp so we can advise on the right finish.
For rush jobs, the fastest route is to upload your print file, choose the closest product, submit your details and share any deadline notes. The sooner we have your artwork and quantity, the faster we can confirm timing and start production.
Useful for CBD businesses, schools, churches, events, NGOs, agencies and corporate teams that need artwork checked before print.
Choose Nairobi CBD pickup or add delivery details during checkout. Countrywide delivery can be coordinated after the order is confirmed.
Small DTF or heat transfer jobs can move faster than embroidery or bulk screen printing. Quantity, artwork readiness and stock determine timing.
Pricing depends on shirt quality, quantity, printing method, artwork size, number of print positions and deadline. DTF is strong for detailed full-colour work, while screen printing is usually better value for bulk simple designs.
Yes. Open the Clothing & Apparel category in our shop to place your order. You can also share your artwork on WhatsApp for review before printing.
For many corporate T-shirts, screen printing is efficient for bulk logo prints, DTF is better for full-colour detailed artwork, and embroidery is best for polos, caps and premium uniforms.
The available product list controls checkout quantities and pricing. For very custom one-off requests, use WhatsApp so the team can confirm garment availability and the right method.